Application Overview
Cement silos are used to store and manage various types of cement powder, each with specific material characteristics. Facilities typically operate multiple silos to accommodate different cement types, with bins fed pneumatically or via air slides from a process or delivery vehicle. The cement is discharged from silos through pneumatic transfer lines, clam shell gates, or slide gates to supply downstream manufacturing processes, bagging systems, or bulk transport trucks and railcars.
Common Challenges in Cement Silo Monitoring
Operators need accurate, continuous level measurement to maintain consistent inventory control, prevent overfilling, and ensure uninterrupted production. Cement powder creates heavy dust, making traditional contact-based sensors unreliable and causing signal interference in harsh conditions.
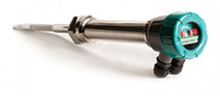
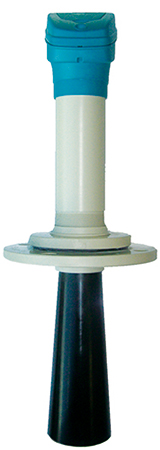
Hawk’s Acoustic Wave Level Sensors provide reliable, non-contact measurement of cement powder levels inside silos. The sensor continuously transmits level data to a control system via analog, relay, or digital communication. As material levels fluctuate, the control system monitors sensor output for real-time inventory management and process control.
These sensors help operators:
- Accurately track material availability and silo capacity
- Automate outlet gate or pneumatic transfer control
- Avoid overfill and low-level conditions with programmable alarms
- Improve safety and reduce downtime in dusty environments
High or low alarm setpoints can be integrated directly into the Acoustic Wave instrument or achieved through redundant point level switches for added protection. Whether your silos feed bulk transport, bagging, or concrete manufacturing lines, Hawk’s level monitoring solutions ensure dependable performance and material flow control.